
For automotive service bays, tyre equipment, pneumatic lifts and body-shop interfaces, use Garage Compressed Air. That guide applies the shared method to automotive work rather than repeating it.
Build a user schedule
List the tools and maintenance tasks that will use compressed air. Obtain their documented flow and pressure requirements, expected duration of use and number operating together. Do not choose a compressor from floor area, employee count or motor power alone.
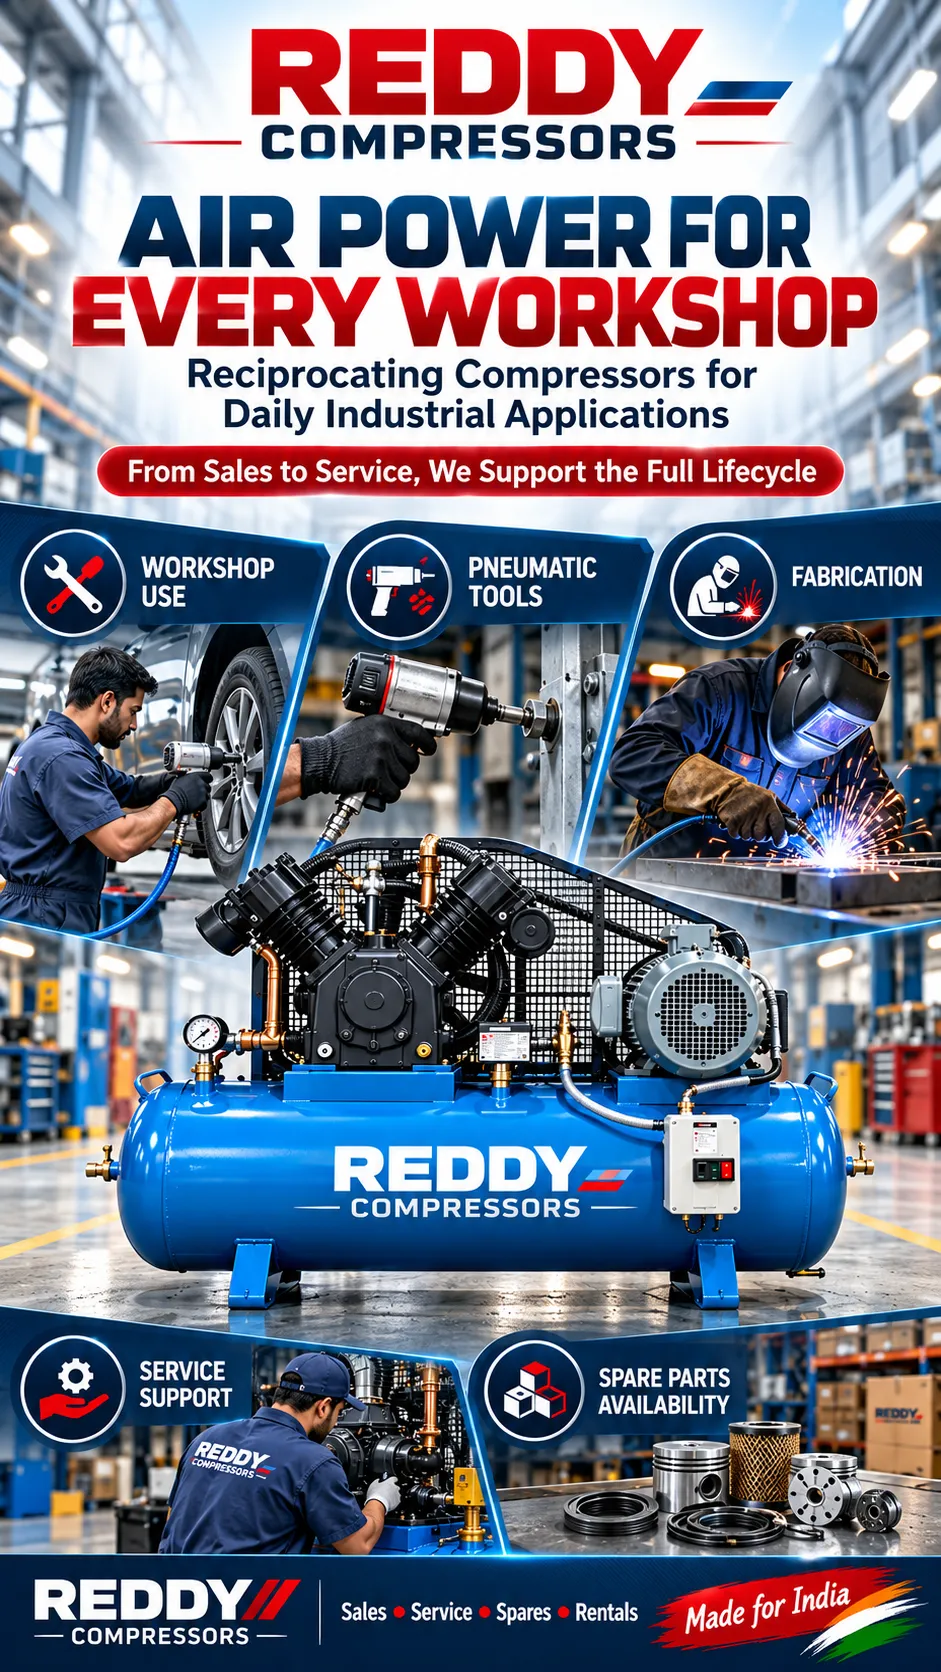
Separate short bursts from sustained loads. Record the working pattern across the shift and identify which combinations create the highest demand. Where usage information is uncertain, plan observations or measurements rather than inserting an arbitrary diversity factor.
User-schedule field | What to record |
|---|---|
Equipment | Tool or process identity |
Air requirement | Documented flow and operating pressure |
Duration | Typical use period and peak duration |
Simultaneity | Other users operating at the same time |
Air quality | Equipment or process requirement |
Location | Outlet and temporary connection route |
Evidence gap | Information still required |
Compare delivered capacity with the operating pattern
Ask for free-air-delivery data with its pressure and reference conditions. Keep the performance basis consistent when comparing proposals. Motor power is useful equipment information, but it is not a substitute for delivered airflow.
Review reciprocating and rotary-screw options against the actual demand pattern and model limitations. Intermittent and sustained operation deserve different questions about duty, controls and service requirements. The label workshop does not establish one universal technology or machine size.
Work back from the tool pressure
Identify the pressure required at each user and consider the equipment between that point and the compressor. Include the receiver connection, treatment, pipework, regulators, hoses and couplings in the review.
If the tool performs poorly, compare conditions at the compressor and the point of use before deciding that more compressor capacity is required. Record the operating state and simultaneous users during the observation. A reading taken under a different demand condition may not explain the complaint.
Give storage a defined purpose
Separate the magnitude of a peak from its duration. Review whether storage is intended to support a brief event, stabilise operation or serve another documented purpose. A receiver does not replace the need for sufficient compressor delivery over the operating cycle.
For a tank-mounted package, check the supplied arrangement against the duty. For separate storage, identify installation and connection responsibilities. Obtain a technically reviewed sizing basis rather than selecting from vessel size alone.
Match air treatment to the users
List equipment requirements rather than describing all workshop air as one quality. General tools and finishing processes may have different needs. Where they do, record the proposed treatment boundaries and the pressure effects of the selected equipment.
Review moisture, filtration and condensate handling together with distribution. Keep treatment selection tied to the actual equipment documents and site conditions. An oil-free compressor label is not, by itself, an acceptance record for painting or another sensitive process.
Include the delivery network
Prepare a simple layout showing the compressor, storage, treatment and outlets. Record pipe and hose routes, fittings, regulators and the planned future users. Investigate restrictions and leakage rather than automatically raising the compressor setting to compensate for poor delivery.
Assess changes using the conditions at the working outlet. Avoid generic hose tables or fixed pressure recommendations without the flow, route and component information needed to support them.
Check installation and access
Review electrical supply, cooling and intake conditions, heat removal and service access against the selected package's instructions. Keep equipment accessible for inspection and planned work. Obtain model-specific start/stop and duty limits instead of applying a universal starts-per-hour rule.
Expansion should be documented as expected new users and operating patterns. Do not add an unexplained percentage margin and assume that it resolves future capacity needs.
Request a workshop system review
Provide the user schedule, current machine details, working hours, layout and any pressure or performance observations. A useful proposal should state its assumptions, equipment scope, installation interfaces and evidence still required.
Workshop air compressors
A workshop is not one air load
A workshop may use compressed air for:
Across brands
Models we supply and service
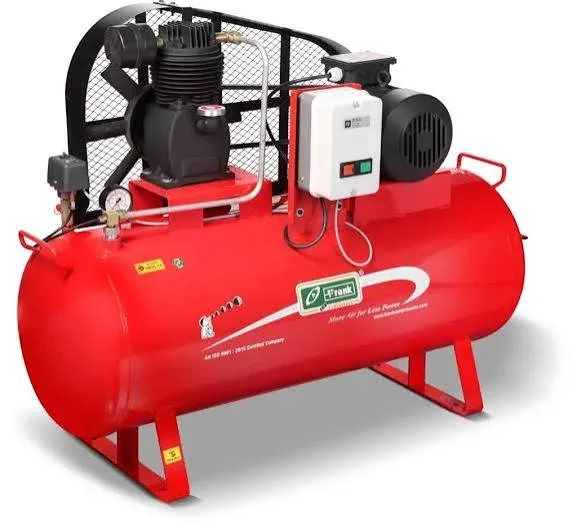
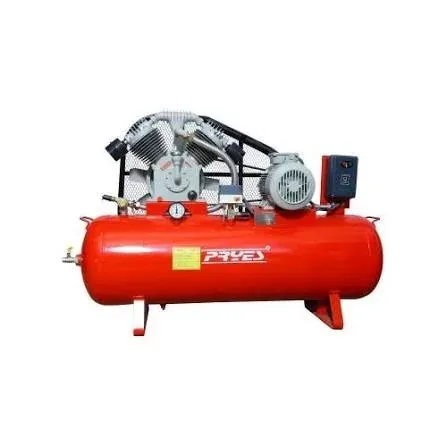
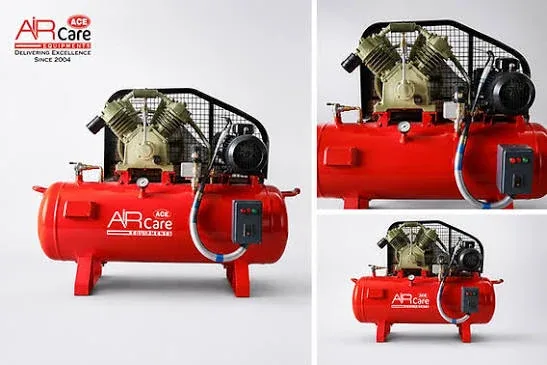
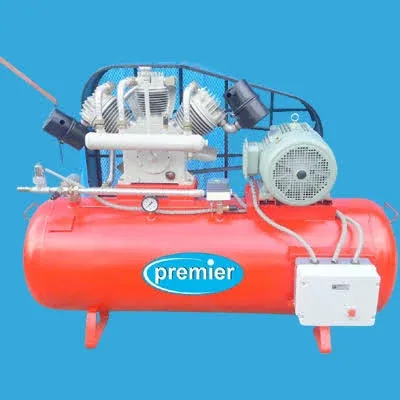
Manufacturer product images, shown to identify machines we sell, service and support. Brand names are trademarks of their owners.
- Pneumatic Tools
- Impact Tools
- Tyre Equipment
- Pneumatic Lifts Where Applicable
- Cleaning
- General Maintenance Systems
It also notes that workshop demand is often intermittent, making the demand profile especially important when choosing between reciprocating and rotary screw compressor technology.
Start with what the workshop actually operates
- “Which HP compressor do workshops normally buy?”
The workshop compressor selection equation
The compressor is one component.
The workshop works from the complete system.
01 — identify every compressed-air user
Create an equipment schedule.
Potential workshop users include:
- Pneumatic Lifts Where Applicable
- Do not size the compressor from workshop floor area alone
- Do not size it from employee count alone
- Do not size it from the compressor already installed
- Start with the users
02 — find the air consumption of each user
Where equipment data are available, establish:
- for each tool or machine
- The correct compressor depends on what will actually be connected
03 — FAD is the capacity number that matters
For compressor comparison, focus on:
Free air delivery — FAD
A larger catalogue CFM number is not enough if the basis is different.
04 — do not buy by motor HP alone
The weak workshop enquiry is:
“I need a 5 HP compressor.”
The stronger enquiry is:
“I need this much delivered air at this pressure for these tools.”
Motor rating is useful equipment information.
It does not independently define usable air capacity.
05 — working pressure must come from the tools
Different workshop equipment may have different pressure requirements.
The important value is:
The minimum pressure required at the point of use
Clearly that compressor discharge pressure and point-of-use pressure are not necessarily the same.
The tool experiences the pressure available at the tool—not the pressure displayed beside the compressor.
06 — the workshop pressure stack
A useful way to think about workshop pressure is:
This follows the source's pressure-stack method.
The goal is to minimise avoidable losses.
Not endlessly increase compressor discharge pressure.
07 — simultaneous use matters
A workshop may own ten pneumatic tools.
That does not necessarily mean all ten operate simultaneously.
But assuming only one will ever run can also undersize the system.
Demand assessment should consider:
- Base Demand
- Intermittent Demand
- Peak Demand
- Leakage
- Future Demand
- Diversity
- That framework is ideal for workshop sizing
08 — ask “how many at the same time?”
This is one of the most important workshop questions.
Two Technicians Using Air Tools Simultaneously?
Tyre Equipment While Another Tool Runs?
Cleaning Air During Other Work?
The answer affects peak FAD.
09 — workshop demand is often intermittent
This.
one of the most important technology-selection variables.
A workshop that uses air for short tool bursts behaves very differently from a production workshop where multiple pneumatic users operate almost continuously.
10 — reciprocating may fit intermittent workshop duty
Workshops as a clear piston-compressor application where:
- Receiver Storage Can Buffer Peaks
- The Compressor Is Not Continuously Loaded
Therefore reciprocating technology may deserve strong evaluation for suitable workshop demand.
Workshop ≠ automatically piston compressor
The load profile still decides.
11 — rotary screw may fit sustained workshop duty
Where workshop air demand becomes:
- High
- Continuous
- Predictable
- Present Across Multiple Shifts
- Rotary screw technology may deserve consideration
So the selection logic is:
Intermittent duty → reciprocating deserves evaluation
Sustained duty → rotary screw deserves evaluation
Neither technology wins automatically.
12 — the load profile decides
This is the master principle.
Do not choose a compressor technology because:
- “Workshops normally use piston compressors.”
- “Rotary screw is more modern.”
13 — receiver storage is particularly relevant to intermittent tools
A correctly selected receiver can help:
- Buffer Short Demand Peaks
- Provide Temporary Stored Air
That can make receiver engineering especially important in workshops with short bursts of high demand.
14 — but storage is not capacity
This very clearly.
Permanently Compensate for Insufficient Compressor Capacity
Repair Major Pressure Drop
A large tank does not make a small compressor a large compressor
15 — peak demand and peak duration should be separated
A short burst from an impact tool is different from a pneumatic machine operating for twenty minutes.
Receiver storage may assist short events.
Sustained load requires sustained compressor output.
This is why the workshop enquiry should ask:
16 — receiver sizing should have a purpose
Receiver-sizing inputs including:
- Compressor Capacity
- System Pressure
- Minimum Acceptable Pressure
- Peak Demand
- Peak Duration
- Control Strategy
- Required Buffer Time
So the right question is not:
“What is the biggest tank available?”
- “What should the receiver accomplish?”
- 17 — tank-mounted piston compressor
For smaller workshops, a receiver-mounted reciprocating package may provide:
- where the actual package matches the duty
- Verify capacity and storage separately
18 — base-mounted + separate receiver
A base-mounted system may deserve evaluation where:
- Larger Storage Is Required
- An Existing Receiver Is Available
- Several Compressors Feed Common Storage
- A Custom Layout Is Needed
- For workshops, do not assume the compact package is always best
19 — workshop air quality is not one specification
A workshop may have several air requirements.
20 — general tool air
General pneumatic tooling may have one set of:
- Actual tool documentation should govern
- Do not automatically treat every workshop user as a sensitive process
21 — paint & finishing air is different
Painting can be sensitive to:
- Moisture
- Oil
- Particles
- Pressure Stability
Therefore paint-air treatment should follow:
22 — do not assume “oil-free compressor” alone guarantees paint-quality air
Paint quality is a system outcome.
It can depend on:
- Compressor Technology
- Moisture Control
- Filtration
- Distribution
- Pressure Stability
- Point-of-Use Condition
23 — tyre equipment may have a different requirement
Use the actual equipment requirement.
24 — pneumatic lifts require equipment-specific data
But it does not provide universal air consumption or pressure.
Verify the lift manufacturer's requirement
25 — impact tools can create short high-demand events
Impact tools are specifically.
The relevant engineering questions are:
- Number of Simultaneous Tools
- not merely the tool's physical size
26 — cleaning air can become a significant load
Cleaning is listed as a workshop-air user.
If cleaning represents meaningful demand, measure or define it as part of the workshop load schedule.
27 — the small-workshop system architecture
A useful workshop chain:
28 — the compressor is only the first component
A workshop can buy a correctly sized compressor and still have:
because the downstream system is poorly designed.
From compressor room to point of use
29 — dryer as required
Dryer selection should be based on:
Required pressure dew point
not compressor size alone.
Workshop = not automatically “no dryer.”
- Workshop = not automatically “dryer required.”
- 30 — filtration as required
Filtration should protect the relevant downstream requirement.
General workshop tools and paint-finishing systems may require different treatment.
The website should avoid one blanket filter package for every workshop.
31 — point-of-use regulation
The workshop-system architecture explicitly includes:
POINT-OF-USE REGULATORS.
This allows different users to receive appropriate pressure where correctly engineered.
But regulators do not eliminate the need for adequate upstream flow.
32 — distribution pipe size matters
Pipework should deliver the required flow without excessive pressure loss.
A compressor with sufficient FAD can still leave tools starved if the distribution system is too restrictive.
33 — do not raise compressor pressure to hide undersized piping
Against trying to solve undersized piping by permanently increasing compressor pressure.
That is a powerful workshop rule.
If tool pressure is low:
Check the distribution first
34 — the source identifies a common workshop error
Buying a larger compressor to solve low tool pressure without checking:
Its instruction is direct:
- This should be one of the page's strongest conversion blocks
- A restrictive hose can reduce usable pressure and airflow at the tool
Evaluate hose selection from:
- Tool Demand
- Length
- Working Pressure
- Connections
- using appropriate engineering/manufacturer data
A system can have adequate pipe diameter but still be restricted by:
- Fittings
- Couplings
- Valves
- Adaptors
- depending on the actual installation
Again, measure the pressure at strategic points before assuming the compressor is undersized.
Leaks become a permanent workshop load whenever the system is pressurised.
If the compressor cycles frequently when tools are not being used:
Leakage should be investigated
Do not automatically increase tank size or compressor capacity.
38 — pressure at the compressor and pressure at the tool should be compared
This is one of the simplest useful workshop tests.
Tool-end pressure under load
A meaningful difference suggests the distribution path deserves investigation.
39 — compressor technology should follow workshop utilisation
A small workshop operating pneumatic tools intermittently is a very different duty from:
- - a body shop spraying continuously
- - a fabrication workshop with several simultaneous air tools
- - an industrial maintenance facility
- - a production workshop operating across multiple shifts
Workshop size alone does not select the compressor
The operating profile does.
40 — reciprocating compressor decision
A reciprocating compressor may be attractive where demand is:
- Characterised by Long Idle Periods
- This can align naturally with many workshop duties
- But actual duty limits still have to be respected
41 — rotary screw decision
Rotary screw may deserve evaluation when workshop demand becomes:
or otherwise behaves more like industrial plant air.
Do not assume a piston machine remains the correct choice simply because the facility is called a workshop.
42 — duty cycle cannot be ignored
Reciprocating equipment can have manufacturer-specific limits involving:
- Loaded Operating Time
- Cooling
- Starts per Hour
- Discharge Temperature
- Pressure
- Environment
Therefore a compressor with adequate CFM may still be wrong for the workshop if expected loaded hours exceed its intended duty.
An intermittent workshop load can lead to frequent cycling if:
- Receiver Storage Is Poorly Matched
- Pressure Band Is Unsuitable
- Manufacturer starting-frequency limits should be respected
- No universal starts-per-hour figure should be published
44 — workshop compressor room
The compressor requires adequate clean cooling and intake air and warns against intake locations drawing:
- Hot Exhaust Air
- Dust
- Process Fumes
- Engine Exhaust
- Excessive Moisture
- Contaminated Air
This is particularly relevant in workshops where welding, engines, grinding or other processes may affect the local environment.
45 — heat must be managed
Most compressor input energy ultimately appears as heat and that poor ventilation can contribute to:
- High-Temperature Alarms
- Lubricant Stress
- Reduced Component Life
- Uncomfortable Maintenance Conditions
- A workshop corner is not automatically a suitable compressor room
Installations should allow practical access for:
- Filter Replacement
- Separator Service
- Oil Service
- Cooler Cleaning
- Motor Inspection
- Belt / Coupling Service Where Applicable
- Electrical Work
A compressor that physically fits behind workshop equipment may still be poorly installed if technicians cannot maintain it safely.
47 — do not hide the compressor where it cannot be serviced
Compactness can tempt a workshop to place the compressor:
- - behind shelving
- - between equipment
- - inside a poorly ventilated room
- - against a wall
The principle is simple:
Provide the access the actual machine requires
48 — air quality for painting should be segmented from general tool air where appropriate
Automotive workshop uses should not automatically receive the same air specification.
Therefore a workshop may need to evaluate:
as different downstream requirements.
This can avoid over-treating every air user while still protecting sensitive operations.
49 — oil-free compressor selection should not be automatic for the entire workshop
- general tools may have one requirement;
- finishing equipment may have another.
The process/equipment specification decides.
Before selecting the compressor, ask:
Will More Bays Be Added?
Will More Technicians Use Pneumatic Tools?
Will Painting Be Added?
Will Operating Hours Increase?
Will New Pneumatic Equipment Be Installed?
Future capacity should be justified.
Against arbitrary oversizing.
51 — do not automatically add a large “safety margin”
Arbitrary excess margin can lead to:
- Inefficient Part-Load Operation
- Workshop growth should be based on credible planned loads—not guesswork
- The compressor has to fit the workshop's actual electrical infrastructure
Before final model selection, verify:
according to current equipment documentation.
53 — no universal workshop compressor size
One Tank Size per Tool Count.
Selection should be based on actual tool demand and duty.
54 — no universal workshop pressure
Likewise, not every workshop should run one standard bar/psi setting.
The actual tools and equipment define pressure requirements.
Then the system should preserve that pressure with minimum avoidable loss.
55 — model data required before product publication
For each workshop compressor recommendation, verify:
- Technology — Reciprocating / Rotary Screw
- Receiver Volume Where Applicable
- Sound Data Where Verified
- No specification should be inferred across product families
56 — customer data to request
For a workshop compressor assessment, collect:
- List of Air Tools / Machines
- Air Consumption of Each Tool if Available
- How Often Each Tool Operates
- Current Tool-End Pressure
If CFM is unknown:
Provide the tool / machine details
The application is enough to begin the selection process.
57 — workshop selection gate
Before choosing equipment, ask:
What tools will use air?
Create the schedule.
What FAD does each require?
Use equipment data where available.
What pressure must reach each user?
Point-of-use pressure matters.
How many users run simultaneously?
Size for realistic peak demand.
Is demand intermittent or sustained?
This influences piston vs rotary screw.
How long does the peak last?
Receiver sizing depends on duration.
What should the receiver do?
Give storage a purpose.
Is painting / finishing included?
Treat its air quality separately.
Are hoses, regulators and fittings restrictive?
Measure before upsizing.
Is ventilation adequate?
Heat must leave.
Can the compressor be serviced?
Provide access.
What expansion is actually planned?
Avoid arbitrary oversizing.
Then select the actual model.
Workshop compressors in one line
A workshop compressor should be selected from the airflow, pressure, simultaneous tool use and duty profile of the actual workshop
With receiver storage, air treatment, hoses, regulators, distribution and ventilation engineered as part of the same system
Do not size the workshop from the compressor
Size the compressor from the workshop
The correct system should define:
The tools
- FAD
- Point-of-use pressure
- Simultaneous demand
- Duty cycle
- Peak duration
- Receiver storage
- Air quality
- Distribution
- Ventilation
- Service access
For smaller workshop systems, it also provides a practical architecture:
COMPRESSOR → RECEIVER → DRYER AS REQUIRED → FILTRATION → DISTRIBUTION → POINT-OF-USE REGULATORS.
And its most important troubleshooting instruction is simple:
Do not buy a larger compressor for low tool pressure before checking hoses, regulators, fittings, leaks and filtration
Compressed air. engineered for uptime
- List the tools
- Verify the FAD
- Define the tool pressure
- Calculate simultaneous use
- Understand the duty
- Size storage with purpose
- Treat the air as required
- Control distribution losses
- Install for cooling & service
- Verify the complete system
- Primary CTA
Request a Workshop Air Compressor Selection
Secondary CTAs
Send Your Tool List for Compressor Sizing
Compare Piston vs Rotary Screw for Your Workshop
Review Receiver Size
Investigate Low Tool Pressure
Review Workshop Dryer & Filtration Requirements