
How a blasting nozzle uses air
In a pressure-blast system, compressed air leaves the compressor, passes through an aftercooler and moisture separator, enters the blast pot, picks up metered abrasive at the mixing valve and accelerates the mixture through the blast hose to the nozzle. The nozzle is the restriction that sets the flow. Its converging inlet and straight or venturi bore convert pressure into velocity, and abrasive particles leave at high speed to clean and profile the surface.
Because the nozzle is effectively a fixed orifice, the air it passes rises with both bore area and upstream pressure. Double the bore and the area, and therefore the air demand, rises roughly four times. Raise the nozzle pressure and flow rises with it, because denser air passes the same opening. This is why two crews quoting “a 375 cfm compressor” can get very different results: one may be running a new No. 6 at 7 bar, the other a worn No. 7 at 5.5 bar.
The useful measure is not how much air the compressor can make with the blast valve closed, but whether it can hold the required pressure at the nozzle while the nozzle is flowing, all shift, in Indian summer ambient conditions.
Typical nozzle air demand by nozzle number
Nozzle numbers describe bore in sixteenths of an inch: a No. 6 has a 6/16 in (3/8 in) bore. The figures below are rounded, typical values drawn from widely published industry charts for new nozzles at about 7 bar (101.5 psig) measured at the nozzle. Individual manufacturers’ charts differ, so always confirm against the chart for the nozzle you will actually use.
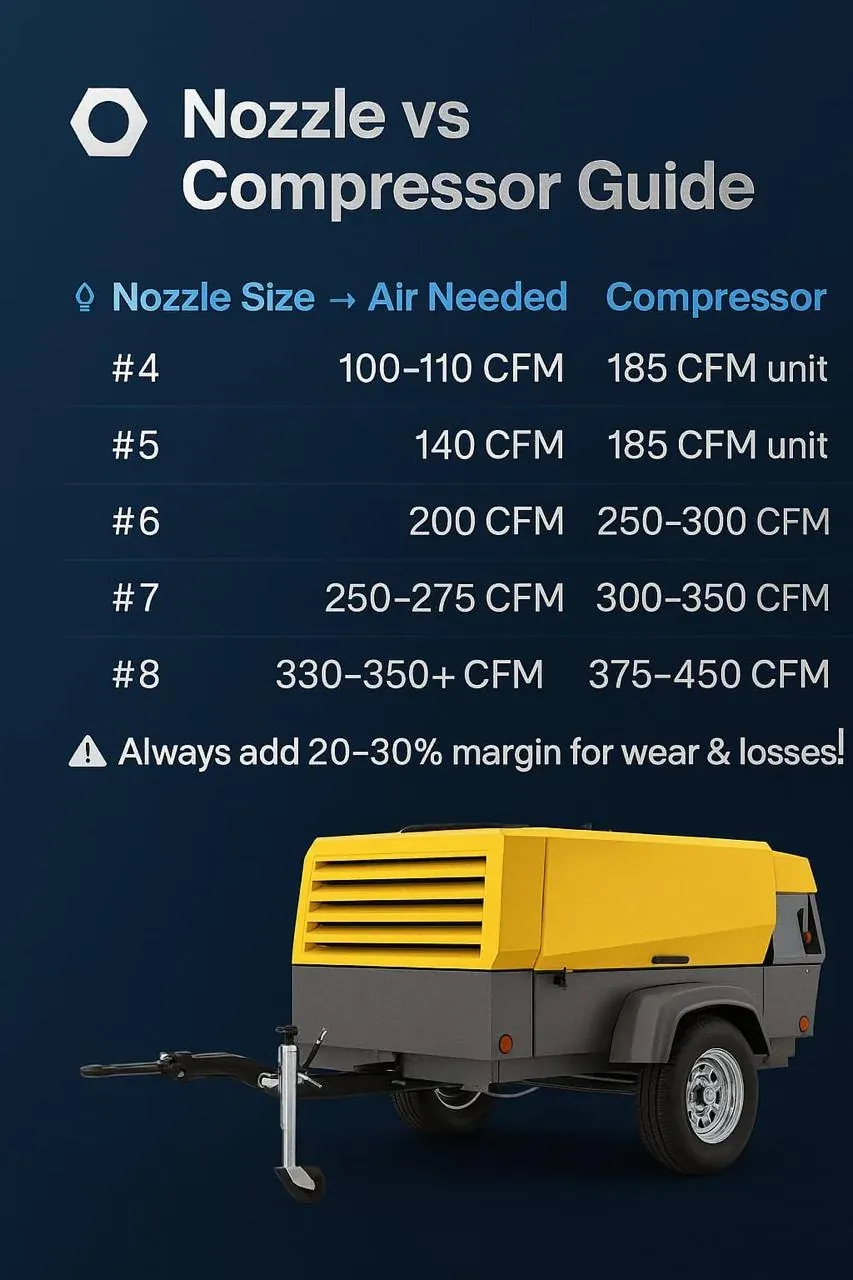
| Nozzle no. | Bore | Typical air at 7 bar (101.5 psig) at nozzle | Typical portable compressor class |
|---|---|---|---|
| No. 3 | 3/16 in (4.8 mm) | about 65–70 cfm | small units, spot repair |
| No. 4 | 1/4 in (6.4 mm) | about 130–140 cfm | 185–250 cfm class |
| No. 5 | 5/16 in (8.0 mm) | about 195–210 cfm | 250–400 cfm class |
| No. 6 | 3/8 in (9.5 mm) | about 280–300 cfm | 375–450 cfm compressor |
| No. 7 | 7/16 in (11.1 mm) | about 380–410 cfm | 400–600 cfm class |
| No. 8 | 1/2 in (12.7 mm) | about 500–540 cfm | 600 cfm class or larger |
Two practical points follow. First, compressor capacity should sit comfortably above the nozzle figure, because the nozzle wears, the pot and hose need some air, and the operator may want a little more pressure. Second, two No. 6 nozzles need about 600–750 cfm of compressor capacity, and one No. 7 plus a small touch-up nozzle puts you at the top of the 400–600 cfm band or above.
Pressure at the nozzle versus pressure at the compressor
Most blasting specifications and nozzle charts assume a working pressure at the nozzle in the region of 6–7 bar (87–101.5 psig). The compressor discharge pressure is always higher than this, because air loses pressure through every component on the way.
- Aftercooler, moisture separator and any filter or dryer in the line.
- The supply hose from compressor to pot, especially if it is long, undersized or has many couplings.
- The blast pot inlet, valves, mixing valve and remote controls.
- The blast hose, which carries abrasive and air together and loses more pressure per metre than a clean air hose.
The only reliable way to know nozzle pressure is to measure it with a hypodermic needle gauge inserted into the blast hose just behind the nozzle while blasting. A loss of 1 bar (14.5 psi) between compressor and nozzle is common on a reasonable set-up; long or undersized hose can lose much more. As a working rule, productivity falls noticeably as nozzle pressure drops, and below about 5.5 bar (79.8 psig) most crews find that profile and cleaning rate suffer badly.
Raising the compressor setpoint to compensate costs fuel. A typical figure in compressed-air practice is about 7% more power for each extra bar of discharge pressure, so fixing hose and fittings is usually cheaper than buying pressure.
Nozzle wear: the hidden air demand
Abrasive erodes the nozzle bore. As the bore opens, air demand rises with the square of the diameter, and the compressor that was adequate on day one starts to fall short. Nozzle pressure drops, the blast pattern widens, and production slows even though the crew sees the compressor running flat out.
- Measure the nozzle bore at the start of the job with a drill-bit gauge or a nozzle orifice gauge, and record it.
- Check bore daily on heavy jobs. A common industry rule is to replace a nozzle once its bore has grown by about 1/16 in (1.6 mm), which is effectively one nozzle number.
- Check the liner for cracks, uneven wear and a damaged entry; a split liner can let abrasive cut the jacket.
- Match the liner material to the abrasive and job length: tungsten carbide for general use, silicon carbide or boron carbide for longer life with aggressive media.
- Size the compressor with an allowance for the nozzle one size larger than you start with, unless nozzles will be changed strictly on schedule.
Hose sizing for blast and supply lines
Undersized hose is the most common reason for low nozzle pressure on hired blasting compressors. A widely used rule is that the blast hose bore should be about three to four times the nozzle bore. For a No. 6 nozzle that means a 1-1/4 in (32 mm) blast hose as a minimum, and a 1-1/2 in hose for long runs or No. 7 and No. 8 nozzles.
| Nozzle | Typical minimum blast hose bore | Typical supply hose, compressor to pot |
|---|---|---|
| No. 4–5 | 1 in (25 mm) | 1-1/2 in (38 mm) |
| No. 6 | 1-1/4 in (32 mm) | 1-1/2 to 2 in (38–50 mm) |
| No. 7–8 | 1-1/4 to 1-1/2 in (32–38 mm) | 2 in (50 mm) or larger |
Keep the supply hose as short and straight as access allows, use full-bore couplings with safety pins and whip checks, and avoid reducing fittings at the pot inlet. Where the pot must be far from the compressor, it is usually better to move the compressor closer or increase the supply hose size than to raise discharge pressure. Hose distribution for larger sites is covered on our temporary air hose and manifold page.
Moisture and oil control for coating quality
Hot compressor discharge air carries a great deal of water vapour. In a humid coastal location or in the monsoon, that water condenses in the hose and pot, makes abrasive clump and choke the metering valve, and leaves moisture on freshly blasted steel that starts flash rust before the primer goes on. Oil-injected screw compressors also carry a small amount of oil aerosol past the separator, which is unacceptable on a surface about to be coated.
- Aftercooler: cools discharge air (typically 75–95 °C at an oil-injected screw airend outlet, lower after the internal cooler) to near ambient so water condenses where it can be removed.
- Moisture separator with automatic drain: removes the bulk liquid water and oil droplets formed in the aftercooler.
- Coalescing filter: recommended where coating specifications demand clean, oil-free air at the nozzle.
- Dryer: a refrigerated dryer (typical pressure dew point around +3 °C) or desiccant unit is justified for high-specification coating work, humid sites or long hose runs.
Surface preparation is usually specified to a recognised standard such as ISO 8501-1 (for example Sa 2½), with profile and cleanliness checks by the coating inspector. Clean, dry air does not by itself achieve the grade, but wet or oily air can make a grade impossible to hold. See portable aftercoolers and portable moisture separators for the equipment we supply with blasting compressors.
Breathing air is a separate system
A blast operator’s supplied-air respirator needs breathing-quality air, delivered through a dedicated breathing-air filtration and monitoring system to its own standard and the respirator maker’s instructions. It must not be treated as a branch off the blast air line. Breathing-air demand per operator is set by the respirator manufacturer and should be added to the total compressor demand. Reddy Compressors can supply the compressed air; the breathing-air purification, carbon monoxide monitoring and respirator system are specialist equipment that the blasting contractor must specify and own.
How to size the compressor for your nozzle
- List each nozzle that will run at the same time, with its number, measured bore and the manufacturer’s chart.
- Read the air demand at your target nozzle pressure, usually around 7 bar (101.5 psig).
- Add an allowance for wear, typically by taking the next nozzle size up, unless replacement is tightly controlled.
- Add the respirator, pot controls and any air tools, vacuum recovery or dust-collector purges.
- Estimate pressure loss from compressor to nozzle and set the compressor working pressure accordingly, usually 8.5–10 bar (123.3–145 psig) discharge for a 7 bar nozzle.
- Choose a compressor that delivers the total at that working pressure, with headroom for high ambient temperature and altitude.
Our abrasive blasting air demand calculator sets this out as a worked table you can fill in for your own job.
How Reddy Compressors helps
Sandblasting air is a core part of our business, not a side line. Over the years we have supplied many compressors for sandblasting, both as outright sales and on hire, to painting, coating and surface-preparation contractors and to plants doing their own maintenance blasting. That experience shapes how we size, equip and service every blasting package we send out.
We sell, rent and service blasting compressors from our base at Tarnaka, Secunderabad, as an independent multi-brand specialist working with ELGi, Atlas Copco, Ingersoll Rand, KAESER, Chicago Pneumatic, Doosan and other makes. Our own rental fleet covers 50–2,000 cfm and 2–30 bar, diesel and electric, and we can send blasting compressors with aftercoolers, moisture separators, supply hoses and, where the specification needs it, dryers.
Our team has supplied air for coating and corrosion-protection contractors at an oil refinery, a petroleum installation at Kurnool and a steel plant in Andhra Pradesh, including round-the-clock duty with operators on shift. Service teams cover all of Telangana and Andhra Pradesh, and we supply compressors and spares across India. For hire details see sandblasting compressor hire.
What to send us
- Nozzle number or bore, nozzle type and how many nozzles will run together.
- Required nozzle pressure and the surface preparation standard specified.
- Blast pot make and size, hose lengths and bores.
- Abrasive type, site location, ambient conditions and coating specification for air quality.
- Respirators and any other air users on the same compressor.
- Duration, shift pattern and whether diesel or electric power is preferred.
Frequently asked questions
What size compressor do I need for a No. 6 sandblasting nozzle?
A new No. 6 (3/8 in) nozzle typically uses about 280–300 cfm at 7 bar (101.5 psig) at the nozzle. Allowing for wear, the respirator and hose losses, most contractors choose a compressor of about 375–450 cfm with a working pressure of 8.5–10 bar (123.3–145 psig). Check the nozzle manufacturer’s chart and measure nozzle pressure on site to confirm the selection.
Why does my blasting compressor run full load but the nozzle is weak?
Usually the nozzle has worn and is now demanding more air than the compressor can supply, or the hose is too small, too long or restricted by fittings. Measure nozzle pressure with a needle gauge while blasting and gauge the nozzle bore. A worn nozzle, a choked moisture separator or a partly closed valve are the common causes. A compressor fault is less likely, though worth checking.
What pressure should a sandblasting nozzle run at?
Most steel surface preparation runs at about 6–7 bar (87–101.5 psig) measured at the nozzle, and nozzle charts are usually based on 100 psig. Delicate substrates or softer media may use less. The compressor discharge must be higher to cover losses through the aftercooler, hoses and blast pot. Measure at the nozzle, not at the compressor gauge, to know what the crew is really getting.
How often should a blasting nozzle be replaced?
Replace the nozzle when its bore has worn about 1/16 in (1.6 mm) larger than new, which is roughly one nozzle number, or when the liner cracks or wears unevenly. Life depends on liner material and abrasive: tungsten carbide suits general work, while silicon or boron carbide lasts longer with hard media. Gauge the bore daily on heavy jobs rather than waiting for production to drop.
Do I need a dryer for sandblasting air?
An aftercooler and moisture separator are the minimum for most blasting, because they remove the bulk of water and oil before the pot. A dryer is worth adding for high-specification coating work, humid coastal sites, monsoon conditions or long hose runs where condensation would cause flash rust or clumped abrasive. The coating specification and inspector’s requirements should decide the air quality needed.
Can I take breathing air from the blasting compressor line?
Not directly. Respirator air must pass through a dedicated breathing-air purification and monitoring system that meets its own standard and the respirator maker’s instructions, including protection against carbon monoxide and oil. The compressor can be the source, but the breathing-air system is specialist equipment owned by the blasting contractor and must be planned separately from the blast air line.
Related pages
Field guide
Blasting performance is decided at the air source
On site a blasting set-up looks simple: a diesel compressor, a hose across the ground, a blast pot and an operator. The finish is decided before the nozzle fires. When the air system is weak the failure is quiet: blasting slows, abrasive use rises, the profile turns uneven, coating adhesion falls and the schedule slips, while the operator keeps working.
Four layers that must all hold
- The compressor’s mechanical condition. A worn machine gives pressure dips under continuous blasting, overheating in hot weather, poor fuel use and unexpected trips. Operator skill cannot make up for unstable air.
- Air quality. Moisture clumps abrasive, blocks nozzles, gives an irregular pattern, weakens coating adhesion and lets steel flash-rust after blasting. Use moisture separation, filtration, working drains and clean receivers.
- The delivery line. Long hoses over rough ground, reused couplings and mismatched bores each add resistance, and resistance is pressure lost. A set rated for high cfm at the compressor can deliver much less at the nozzle: slower blasting, more fuel, more labour hours and more abrasive. Treat the hose line as a pipeline.
- The blast pot. Metering valves, seals and pot design decide whether abrasive feed is steady. A worn pot gives a fluctuating pattern even from a perfect compressor.
Size for the nozzle you will have
Air demand follows nozzle diameter, nozzle wear, pressure, the number of operators and the hose size and length. As a nozzle wears its bore grows and it draws more air, so a compressor that suited a new nozzle can become short as it wears. Measure at the nozzle, not at the compressor gauge. Use the blasting air demand calculator, which has a worked example, and see temporary air for blasting.
Indian site conditions
- Summer heat stresses cooling systems.
- Monsoon humidity puts more water into the air line.
- Dusty construction zones load filters quickly.
- Moving between sites speeds up wear on hoses and couplings.
Equipment and hose choices should be made for those conditions rather than for a brochure’s controlled environment.
The slow cost of a weak air system
Longer projects, more abrasive, more fuel, extra labour hours, rework, coating failures and downtime rarely arrive as one big failure. They add up quietly, and across projects can exceed the price of a better set-up. If blasting feels slower than it should, abrasive use is high or coatings fail later, check the air system before blaming operator technique.
Calculators and worked examples
These tools give indicative figures for screening, comparison and for preparing an enquiry. They run in your browser and send nothing. No prices or tariffs are assumed: enter your own to see costs. Efficiencies and other figures shown are example values: replace them with your own. Results are not a performance guarantee or a design certificate; final selection is confirmed by a service engineer against the machine data sheet and the site.
Abrasive blasting air demand
Estimate the air a blast nozzle takes, so the compressor and hose can be chosen to hold pressure at the nozzle.
The worked example below shows the method with fixed numbers. Turn on JavaScript to change the inputs.
Worked example
Inputs
- Nozzle bore (mm): 8
- Pressure at the nozzle (bar g): 7
- Discharge coefficient: 0.9
- Number of nozzles: 1
- Allowance for pot, hose and leaks (%): 10
Result
- Air demand, new nozzle: 4.69 m³/min = 166 cfm
- Nozzle number (bore in 1/16 inch): 5
- Air demand when worn one size (1/16 in larger bore): 6.74 m³/min = 238 cfm: size the compressor for this, then replace the nozzle
Method. Nozzle air treated as orifice flow at the nozzle pressure: free air = Cd × A × choked mass flow ÷ ρ₀. Venturi nozzles with an effective Cd near 0.9 are typical; use the supplier value. Add flow for the pot and for leaks. Nozzle numbers are the bore in sixteenths of an inch (No. 6 = 3/8 in = 9.5 mm). A nozzle wears larger in use, so size the compressor for the nozzle worn one size and replace it at that point.
What to take from it. A worn nozzle passes more air for less work. Check bore wear and keep the pressure at the nozzle, not at the compressor.
Technical content reviewed by D. Srinivas Reddy, Managing Partner and service engineer, Reddy Compressors. Last updated 17 October 2026. How our engineering content is reviewed.