
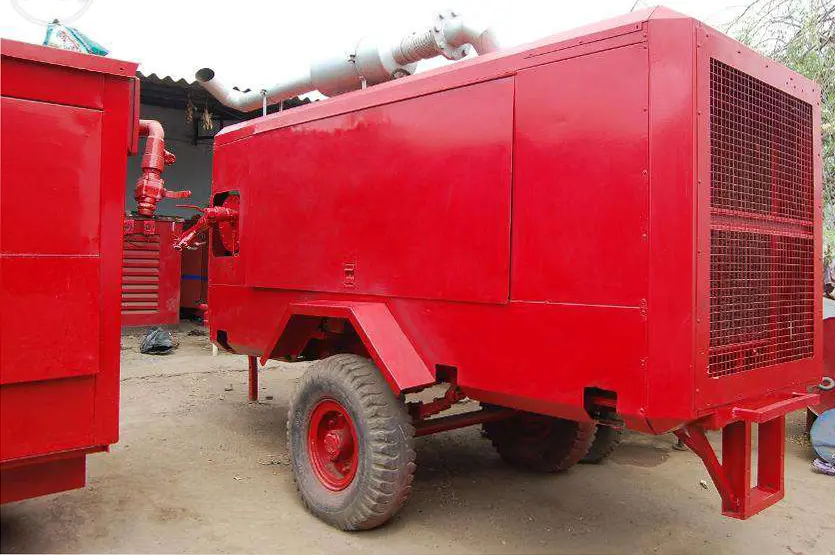
When blasting contractors hire air
Abrasive blasting is one of the heaviest continuous loads a portable compressor can face: the nozzle is open for most of the shift and the compressor runs near full load. Contractors hire rather than buy for several reasons.
- A project needs more nozzles, or larger ones, than the contractor’s own fleet supports.
- A refinery, power plant or steel plant shutdown compresses coating work into a short, intensive window.
- Painting and corrosion-protection contracts on tanks, pipelines, bridges and structures are seasonal or one-off.
- The owned compressor is down for overhaul and the job cannot stop.
- The site needs electric compressors to avoid diesel exhaust in an enclosed area, or diesel units because no power is available.
This page covers compressed-air abrasive blasting for surface preparation, not explosive blasting in quarries or mines.
Sizing temporary air from the nozzle
The nozzle sets the demand. As typical industry figures for new nozzles at about 7 bar (101.5 psig) at the nozzle: a No. 5 uses about 195–210 cfm, a No. 6 about 280–300 cfm, a No. 7 about 380–410 cfm and a No. 8 about 500–540 cfm. Worn nozzles use more. Detail and wear rules are on our nozzle and air supply page.
| Blasting set-up | Typical compressor class | Typical working pressure |
|---|---|---|
| Spot repair, one No. 3–4 nozzle | 185–250 cfm (about 5.2–7.1 m³/min) | 7 bar (101.5 psig) |
| One No. 5–6 nozzle | 250–450 cfm; about 375–450 cfm for a No. 6 | 8.5–10 bar (123.3–145 psig) |
| One No. 7 nozzle, or two No. 5 | 400–600 cfm (about 11.3–17 m³/min) | 8.5–10 bar (123.3–145 psig) |
| One No. 8, or two No. 6–7 nozzles | 600–900 cfm or two compressors | 8.5–10 bar (123.3–145 psig) |
| Multi-crew tank or structure job | 900–2,000 cfm station, several units on a manifold | to suit nozzles and hose runs |
The compressor must deliver its rated flow at the working pressure in site conditions. In an Indian summer, with ambient temperatures of 40–45 °C, and above 45 °C on open sites, a compressor’s cooling system and its high-temperature shutdown margins matter as much as its nameplate cfm. Check the air demand calculator to work through your own numbers.
Diesel or electric for blasting work
Diesel portable compressors are the default for blasting, because most coating jobs are outdoors, remote from a suitable power supply and move around the site. Electric compressors suit long jobs inside a plant where power is available and diesel fumes or fuel handling are a concern, such as a blasting shop or a workshop bay with extraction. The trade-offs are covered on our diesel or electric rental air page.
- Diesel: independent of site power, towable, needs refuelling, fuel storage and spill control.
- Electric: no fuel logistics, quieter, needs a correctly sized supply, cable and starter.
- Either: needs ventilation, shade where possible and protection from abrasive dust drawn into the air intake and cooler.
Air treatment for coating quality
Blasting is usually followed directly by coating, and moisture or oil on a freshly blasted surface leads to flash rust and poor adhesion. Temporary air for blasting therefore normally includes a treatment train.
- Aftercooler sized for the full compressor flow, bringing discharge air close to ambient.
- Moisture separator with a working drain, positioned near the blast pot.
- Coalescing filtration where the coating system requires clean, oil-free air.
- Refrigerated dryer (typical pressure dew point about +3 °C) or desiccant dryer for humid coastal sites, monsoon conditions or high-specification linings.
Surface preparation grades such as ISO 8501-1 Sa 2½ are set by the coating specification and confirmed by the coating inspector. Air treatment helps the crew hold the grade; it does not replace correct abrasive, technique and inspection. See temporary air treatment trains.
Hoses, distribution and the blast pot
A hire package is only as good as its hose route. Undersized or very long supply hose is the most frequent cause of low nozzle pressure on site. Typical practice is a 1-1/2 to 2 in (38–50 mm) supply hose to each pot, a blast hose about three to four times the nozzle bore, full-bore couplings with safety pins and whip checks, and a manifold with individual isolation valves when one compressor feeds several pots.
The compressor’s maximum pressure must not exceed the blast pot’s rating unless a correctly rated regulator and relief device protect it. Interface details are on our blast pot and compressor interface page.
Site set-up and running the job
- Place the compressor upwind of the blasting area and away from abrasive dust and spent media.
- Give the compressor clear space for cooling air; do not box it in with sheeting.
- Level the unit, chock the wheels and keep the towbar clear of traffic routes.
- Provide bunded fuel storage and a refuelling routine that suits the shift pattern.
- Agree who starts, stops and monitors the compressor, and who drains separators.
- Record pressure at the compressor, at the pot and at the nozzle on the first day.
On round-the-clock jobs, maintenance has to be planned around production. On our own hire jobs we change oil and service at every 300 running hours, and on continuous work we schedule that service at shift change so that blasting is not interrupted.
Daily checks during a blasting hire
- Engine oil, coolant and fuel levels before the first start of each shift.
- Air filter restriction indicator, which rises quickly in abrasive dust.
- Cooler cores, cleaned with low-pressure air if dust has built up.
- Aftercooler and separator drains, confirmed to be discharging.
- Discharge temperature and pressure readings, logged against the first-day figures.
- Hose condition, couplings, safety pins and whip checks.
A rising discharge temperature or a falling nozzle pressure is an early warning; tell us before it becomes a shutdown.
Breathing air and safety boundaries
The blast operator’s supplied-air respirator needs breathing-quality air through a dedicated purification and carbon monoxide monitoring system to its own standard. That system belongs to the blasting contractor; we can supply the compressed air feeding it and include its demand in sizing. Compressed-air safety on site, including hose restraint, isolation, depressurisation before uncoupling and exclusion zones around the nozzle, follows the client’s and contractor’s procedures.
Project experience
Blasting compressors are one of the duties our fleet and service teams handle most often, for sales and hire alike, so the issues described on this page, from wet abrasive and worn nozzles to undersized hose and summer overheating, are ones our engineers deal with routinely on real jobs. Our team, across Reddy Generators and Reddy Compressors, has provided air for industrial coating and corrosion-protection contractors at an oil refinery and a petroleum installation at Kurnool. On one urgent steel-plant coating job in Andhra Pradesh we supplied a 450 cfm diesel portable compressor on round-the-clock duty, with skilled operators on 12-hour shifts, maintenance in our scope, oil changes every 300 hours and breakdown support.
How Reddy Compressors helps
Sandblasting air is a core part of our business, not a side line. Over the years we have supplied many compressors for sandblasting, both as outright sales and on hire, to painting, coating and surface-preparation contractors and to plants doing their own maintenance blasting. That experience shapes how we size, equip and service every blasting package we send out.
We rent, sell and service blasting compressors from our office at Tarnaka, Secunderabad, as an independent multi-brand specialist working with ELGi, Atlas Copco, Ingersoll Rand, KAESER, Chicago Pneumatic, Doosan and other makes. Our own fleet covers 50–2,000 cfm and 2–30 bar, diesel and electric, with aftercoolers, moisture separators, dryers and hoses. We can provide operators, servicing on hire and breakdown support, and for long-term projects we can supply brand-new compressors to site.
Service teams cover all of Telangana and Andhra Pradesh; equipment and rentals are supplied across India, with project-based site support where feasible. Start with sandblasting compressor hire or our temporary air engineering centre.
What to send us
- Number of nozzles, nozzle numbers and target nozzle pressure.
- Blast pot make and pressure rating, hose lengths from compressor to pot.
- Coating specification and required air quality.
- Site location, access, power availability and ambient conditions.
- Duration, hours per day and whether operators are needed.
- Any respirators, air tools or dust-collector purges on the same supply.
Frequently asked questions
What size compressor should I hire for sandblasting?
Size it from the nozzle. One No. 6 nozzle typically needs about 280–300 cfm at 7 bar (101.5 psig) at the nozzle, so a 375–450 cfm compressor working at 8.5–10 bar (123.3–145 psig) is a common choice. Two No. 6 nozzles usually need 600–750 cfm. Add respirator air and an allowance for nozzle wear before choosing.
Does a hired blasting compressor come with an aftercooler?
For blasting we normally recommend an aftercooler and moisture separator as part of the package, because hot, wet air causes abrasive clumping and flash rust. Dryers and coalescing filters can be added where the coating specification asks for drier or cleaner air. Tell us the coating system and site conditions and we will propose a suitable treatment train with the compressor.
Can I hire an electric compressor for blasting?
Yes, where the site has a suitable power supply and the work stays in one area for a reasonable time, such as a blasting bay or plant workshop. Electric units avoid diesel exhaust and refuelling. They need correctly sized cable, protection and starting arrangements, which the site’s electrical team should confirm. For outdoor or moving work, diesel portables are usually more practical.
Who maintains the compressor during a blasting hire?
On our hire jobs, compressor servicing is normally in our scope: we change oil and service at 300 running hours and attend breakdowns. Daily checks such as fuel, separator drains and visual inspection are agreed with the site or covered by our operators where we supply them. The blast pot, respirators and blasting equipment remain the contractor’s responsibility.
Why is my hired compressor not keeping up with the blasting crew?
Check nozzle pressure with a needle gauge while blasting. Common causes are worn nozzles drawing more air than planned, undersized or very long hose, a restricted separator or valve, an extra crew added to the same compressor, or high ambient temperature limiting output. Send us the nozzle sizes, pressures and hose details and we can tell whether a larger compressor or a better hose route is needed.
Can you supply blasting compressors outside Telangana and Andhra Pradesh?
Yes. Compressors, rental packages and spares are supplied across India, and project-based site support is arranged where it is feasible. Our service teams are based for regular coverage across Telangana and Andhra Pradesh. For projects in other states, send the location, duration and duty and we will propose how mobilisation, servicing and support will work.
Related pages
Calculators and worked examples
These tools give indicative figures for screening, comparison and for preparing an enquiry. They run in your browser and send nothing. No prices or tariffs are assumed: enter your own to see costs. Efficiencies and other figures shown are example values: replace them with your own. Results are not a performance guarantee or a design certificate; final selection is confirmed by a service engineer against the machine data sheet and the site.
Abrasive blasting air demand
The worked example below shows the method with fixed numbers. Turn on JavaScript to change the inputs.
Worked example
Inputs
- Nozzle bore (mm): 8
- Pressure at the nozzle (bar g): 7
- Discharge coefficient: 0.9
- Number of nozzles: 1
- Allowance for pot, hose and leaks (%): 10
Result
- Air demand, new nozzle: 4.69 m³/min = 166 cfm
- Nozzle number (bore in 1/16 inch): 5
- Air demand when worn one size (1/16 in larger bore): 6.74 m³/min = 238 cfm: size the compressor for this, then replace the nozzle
Method. Nozzle air treated as orifice flow at the nozzle pressure: free air = Cd × A × choked mass flow ÷ ρ₀. Venturi nozzles with an effective Cd near 0.9 are typical; use the supplier value. Add flow for the pot and for leaks. Nozzle numbers are the bore in sixteenths of an inch (No. 6 = 3/8 in = 9.5 mm). A nozzle wears larger in use, so size the compressor for the nozzle worn one size and replace it at that point.
What to take from it. A worn nozzle passes more air for less work. Check bore wear and keep the pressure at the nozzle, not at the compressor.
Technical content reviewed by D. Srinivas Reddy, Managing Partner and service engineer, Reddy Compressors. Last updated 17 October 2026. How our engineering content is reviewed.