
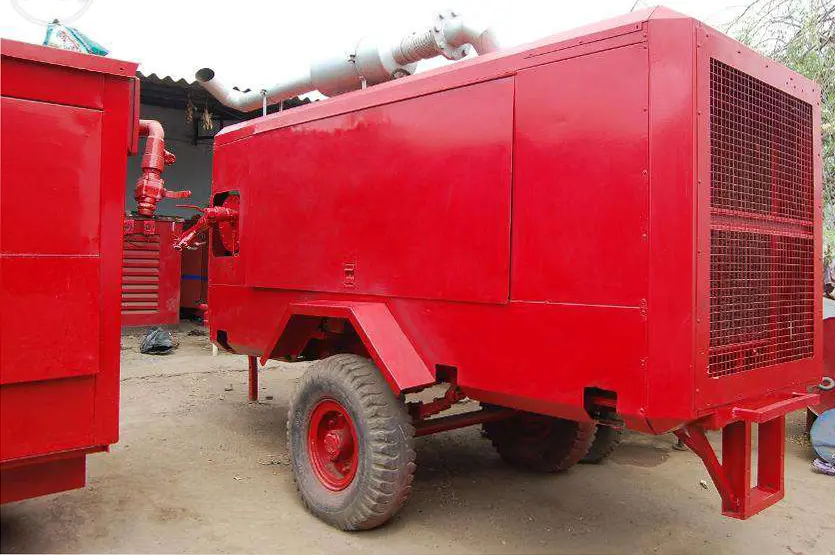
Why fuel is part of the air-supply design
A diesel portable compressor can have the right flow and pressure and still stop production because nobody planned how fuel would get to it. On round-the-clock jobs, the tank may need refilling every shift. On remote sites, the delivery vehicle may not reach the machine in the monsoon. Fuel planning turns a nominal tank size into a reliable number of operating hours.
Start with the role of the diesel package. A machine that is the only air source needs a different fuel plan from one that tops up peak demand or stands by for a breakdown. The consequence of a missed refill is also different, so continuity needs drive how much margin to carry.
Count every fuel-dependent machine
A temporary air station may include more than one diesel engine. A diesel compressor may run alongside a generator powering the dryer, lighting and controls. An electric compressor may depend entirely on a DG set. Include every fuel user in the plan, otherwise the compressor may have fuel while the generator feeding its dryer runs dry, and the air quality fails instead of the air supply.
Estimating fuel consumption
Diesel consumption depends on engine load, which depends on the air actually drawn, the discharge pressure and the ambient conditions. A compressor running fully loaded at high pressure uses much more fuel per hour than the same machine idling or unloaded. Typical litres per hour therefore depend on load; there is no single figure for a compressor size.
- Obtain the maker’s fuel consumption data for the selected model at relevant load points and pressure.
- Estimate the load profile: hours at full load, part load and unloaded per shift.
- Combine them into an expected consumption per shift and per day.
- Check the estimate against actual readings in the first days of hire and adjust.
Pressure has a direct effect: about 7% more power, and therefore roughly proportionally more fuel, for each extra bar of discharge pressure. Running a compressor at 10 bar (145 psig) when the work needs 7 bar (101.5 psig) burns fuel for nothing. High ambient temperatures and dust-loaded coolers also raise engine load through fan demand and reduced efficiency.
From tank size to usable endurance
Nominal tank capacity is not usable fuel. Allow for:
- A reserve that should never be drawn on in normal operation, so the engine does not ingest sediment or air.
- The time it takes to arrange and complete a refill.
- Variation in consumption between shifts and days.
- Delays in fuel delivery, especially on weekends, holidays and during heavy rain.
Usable endurance is the usable volume divided by the expected consumption rate. Compare it with the refuelling interval you can reliably achieve. If endurance is shorter, add an external tank, increase refuelling frequency or plan a changeover to another compressor during refuelling.
Refuelling arrangements compared
| Arrangement | Suits | Points to manage |
|---|---|---|
| Machine tank, manual refill from cans or barrels | Short jobs, low hours, single machine | Spillage, contamination, labour, records |
| Site bowser or mobile tanker | Several machines, daily refills | Vehicle access, scheduling, metering |
| External bulk tank connected to the machine | Round-the-clock hire, remote sites | Bunding, approved connection, siting rules |
| Fuel supplier delivery to site tank | Long projects, high consumption | Reliable supply contract, delivery windows |
Where external tanks or bulk storage are used, the site’s rules for fuel storage, bunding, fire safety and separation distances apply. Connections to a compressor’s fuel system must follow the maker’s instructions.
Refuelling safely without stopping the air
Many compressor makers require the engine to be stopped for refuelling. If the air cannot stop, plan for it:
- Run two machines so one carries the load while the other is refuelled.
- Use an external tank so refuelling the tank does not involve the machine.
- Schedule refuelling at low-demand times or planned breaks.
- Provide a receiver large enough to ride through a short changeover where demand allows.
During refuelling, keep ignition sources away, use spill trays and absorbents, and never refuel a hot engine where fuel could contact exhaust surfaces. Follow the site’s fuel-handling procedures.
Keeping fuel clean
Dirty or wet diesel blocks filters, damages injectors and stops engines. In Indian conditions, dust and monsoon humidity are constant risks.
- Buy from reliable sources and keep containers clean and closed.
- Use filters or funnels with mesh when transferring fuel.
- Drain water separators on the machine as part of daily checks.
- Keep spare fuel filters on site for long, high-hour hires.
- Do not leave storage containers open to rain and dust.
Low fuel also matters: running a tank close to empty draws sediment and air into the system, causing hard starting and stops. If an engine runs out of fuel, it may need its fuel system bled before restarting.
Storage on site needs the same care. Keep drums and tanks shaded, raised off the ground and closed, because summer heat of 40–45 °C, and above 45 °C on open sites, speeds up fuel ageing and condensation forms inside part-filled tanks as temperatures swing between day and night. Use the oldest fuel first, avoid storing more than the hire will use, and check stored fuel for water before transferring it. On long hires through the monsoon, inspect the machine’s fuel filler cap seal and tank breather, since rain entering a poorly sealed tank is a frequent cause of water in the fuel system.
Records that prevent problems and disputes
A simple fuel log protects both the plant and the supplier. Record date, time, hour-meter reading, litres added and who refuelled. Over a few days, the log shows actual consumption per running hour, warns of abnormal use that may signal a fault or leakage, and supports planning of deliveries. It also gives evidence for the commercial terms if fuel is supplied by one party and consumed on behalf of another.
Who supplies the fuel?
Agree at the start who buys fuel, who refuels, who checks levels and how fuel is accounted for at the end of the hire. Common arrangements are customer-supplied fuel with the rental supplier’s operators refuelling, or fuel supplied by the rental company and charged on an agreed basis. Record the fuel level at delivery and at return, ideally with a photo of the gauge or a dip reading, so the closing account is clear.
Fuel planning on round-the-clock hire
Continuous jobs show why planning matters. On one hire, our team ran a 450 cfm diesel compressor round the clock for a coating contractor at a steel plant in Andhra Pradesh, with operators on 12-hour shifts, oil changes every 300 hours and maintenance in our scope. On jobs like this, the shift change is the natural point for fuel checks, water-separator draining and a log entry, so refuelling becomes routine rather than an emergency.
How Reddy Compressors helps
Reddy Compressors rents diesel portable compressors from its own fleet, from small site machines to high-pressure drilling units, within a fleet range of 50–2,000 cfm and 2–30 bar (29–435.1 psig). We also sell new and used compressors and service ELGi, Atlas Copco, Ingersoll Rand, KAESER, Chicago Pneumatic, Doosan and other brands as an independent multi-brand specialist, not an authorised dealer. We have tie-ups with all major and reputed brands.
For diesel hires, we can share the maker’s consumption data for the proposed machine, help estimate fuel per shift, advise on tank and refuelling arrangements, and provide operators who keep fuel and service logs. Hire machines are serviced every 300 running hours. Where generators are also needed, Reddy Generators, under the same management, can supply them. Our office is at Tarnaka, Secunderabad; our service team covers Telangana and Andhra Pradesh, and we supply across India. Use the temporary air fuel logistics calculator for a first estimate.
What to send us
- Air flow and pressure needed, and hours per day.
- Whether the compressor is the only source, a peak supplement or standby.
- How fuel will be supplied and who will refuel.
- Site access for fuel delivery, including in monsoon.
- Any site rules for fuel storage and handling.
- Other diesel equipment, such as generators, in the same station.
Frequently asked questions
How much diesel does a portable air compressor use per hour?
It depends on load, discharge pressure, engine and conditions, so there is no single figure for a compressor size. A machine running fully loaded at high pressure uses far more fuel than the same machine running unloaded. Ask for the maker’s consumption data for the specific model, estimate your load profile, then check actual consumption from hour-meter and refuelling records during the first days of hire.
How often should a diesel rental compressor be refuelled?
Often enough that usable fuel never falls below a safe reserve. Work out usable endurance from tank volume, reserve and expected consumption, then compare it with how reliably you can refuel. On round-the-clock jobs, refuelling at each shift change is common. On remote or monsoon-affected sites, an external tank or extra margin helps avoid running dry.
Can I refuel a diesel compressor while it is running?
Follow the maker’s instructions and site rules; many require the engine to be stopped. If the air supply cannot be interrupted, use a second compressor to carry the load during refuelling, an external tank, or a receiver to ride through a short stop. Keep ignition sources away, use spill trays, and never let fuel contact hot exhaust parts.
Why does running at higher pressure increase fuel use?
The engine has to do more work to compress air to a higher pressure. As a rule of thumb, each extra bar of discharge pressure needs about 7% more power, and fuel use rises roughly in line. Setting the compressor to the pressure the work actually needs, plus real hose losses, is one of the simplest ways to cut fuel use on a hire.
What happens if a diesel compressor runs out of fuel?
The engine stops and the air supply is lost. Running dry can also draw sediment and air into the fuel system, so the system may need bleeding and filters may need changing before the engine restarts reliably. A refuelling schedule, a fuel log and a low-fuel reserve that is never touched in normal operation prevent this.
Who pays for fuel on compressor hire in India?
That is set by the hire agreement. Often the customer supplies fuel and the supplier’s operators refuel and keep logs; other arrangements are possible. Whatever is agreed, record fuel level at delivery and return, and log every refill with hour-meter readings so both sides can reconcile consumption at the end of the hire.
Related pages
Calculators and worked examples
These tools give indicative figures for screening, comparison and for preparing an enquiry. They run in your browser and send nothing. No prices or tariffs are assumed: enter your own to see costs. Efficiencies and other figures shown are example values: replace them with your own. Results are not a performance guarantee or a design certificate; final selection is confirmed by a service engineer against the machine data sheet and the site.
Temporary air fuel logistics
The worked example below shows the method with fixed numbers. Turn on JavaScript to change the inputs.
Worked example
Inputs
- Number of machines: 2
- Loaded hours per machine per day: 14
- Fuel burn when loaded (L/h): 40
- Unloaded hours per machine per day: 4
- Fuel burn when unloaded (L/h): 12
- Stopped hours in the working day: 2
- Tank size, nominal (L): 500
- Filled to (% of tank): 95
- Never run below (% of tank): 10
- Possible delivery delay (days): 2
- Days between deliveries: 7
Result
- Fuel per machine per day: 608 litres
- Fuel for the site per day: 1,216 litres
- Full-load burn × clock hours, for comparison: 1,600 litres a day (32% higher)
- Usable fuel per tank: 425 litres
- Average burn while running: 33.8 L/h
- Tank autonomy: 12.6 running hours
- Refuels per machine per day: 1.4 on average (plan 2 visits on a full day)
- Delay reserve: 2,432 litres
- Order per delivery: 10,944 litres, less fuel already on site
- Fuel cost per delivery period: Enter your diesel price (cost per litre) above
Method. Fuel per machine per day = loaded hours × loaded burn + unloaded hours × unloaded burn (stopped hours use none). Usable tank = tank × (fill level − lowest level). Autonomy = usable tank ÷ average burn while running. Weekly order = days × site litres a day + delay reserve, less fuel already on site. Take burn rates from the supplier datasheet for the actual load.
What to take from it. Full-load burn multiplied by clock hours overstates fuel. Plan refuelling at shift changes, and size site storage before deciding delivery frequency.
Technical content reviewed by D. Srinivas Reddy, Managing Partner and service engineer, Reddy Compressors. Last updated 17 October 2026. How our engineering content is reviewed.